A coil pipe assembly is easy to overlook because much of its work happens inside a flexible endoscope. Yet its geometry, flexibility, interfaces, and surface condition can affect mechanical support and the way neighboring components move. For repair centers, understanding the part before ordering is more reliable than choosing a replacement by photograph alone.
This article explains the purchasing and inspection questions that matter most. Construction varies among endoscope types and models, so qualified personnel should always use the correct service documentation and manufacturer instructions for use (IFU).
What Is an Endoscope Coil Pipe Assembly?
A coil pipe assembly is a flexible, helically formed component used as part of an internal mechanical structure or pathway. Depending on the design, it may support controlled flexibility, protect or guide internal elements, maintain a defined path, or connect to adjacent fittings. It should not be confused automatically with an insertion tube, a biopsy channel, or a light guide tube.
The term “coil pipe” can cover visibly similar parts with different dimensions and end connections. Even when two assemblies share a comparable outer appearance, differences in diameter, pitch, length, stiffness, fitting geometry, or material can prevent correct installation.
Where It Fits in the Mechanical System
A flexible endoscope contains several nested and interacting components. The coil pipe assembly does not work in isolation: it may sit near channels, cables, wiring, optical elements, protective sheaths, and connection fittings. Its routing and movement therefore have to be considered as part of a system. A dimensionally incorrect part can create interference even when the coil itself appears to fit the available space.
Before removal, document the original route, connection orientation, transition positions, and relationship to neighboring parts. Clear photographs from several angles can prevent uncertainty during reassembly. If the service procedure defines reference marks or an installation direction, preserve and follow them.
Why Coil Geometry Matters
The helix is not merely a visual feature. Wire or strip dimensions, coil pitch, winding consistency, inner and outer diameter, and transition areas influence how the component bends and interfaces with the rest of the device. A replacement that is too stiff may restrict movement or increase stress at its connection points. A part that is too flexible may not provide the intended support.
Do not stretch, compress, trim, or reshape a replacement to make it fit unless the model-specific procedure explicitly permits that operation. Such changes can alter performance and may move the work beyond ordinary servicing.
Pitch and Winding Direction
Coil pitch describes the spacing and progression of the helical turns. A compact pitch and an open pitch can respond differently to bending, compression, and torsion. Winding direction can also influence how the component behaves when connected or routed. These features should be treated as specifications, not cosmetic details.
Measure pitch over a defined number of turns rather than judging a single gap, especially when the part is flexible. The component should rest naturally and should not be stretched for the measurement unless the approved drawing or method specifies a controlled condition.
Transitions and End Fittings
Many failures begin at a transition rather than in the middle of the coil. The point where the helix meets a sleeve, connector, tube, or termination can concentrate stress. Inspect these areas for separation, cracking, loose joints, sharp edges, incomplete bonding, or a sudden change in alignment.
End fittings should be compared by more than their outer shape. Check insertion depth, shoulder location, bore, thread or attachment features, orientation, and the surface that mates with the next component. A small difference can change working length or place stress in the wrong location.
Common Wear and Damage Indicators
Inspection should be based on documented acceptance criteria. Potential rejection indicators may include permanent kinks, localized flattening, nonuniform pitch, broken or raised coil edges, corrosion, contamination that cannot be removed by the approved process, loose fittings, or deformation at transition points.
Also examine the surrounding assembly. A damaged coil may be the result of incorrect routing, repeated excessive bending, impact, a misaligned fitting, or interference from another component. If the root cause remains, a new coil pipe assembly can be damaged again.
Distinguishing Normal Curvature From Permanent Deformation
A flexible coil pipe may adopt a gentle curve when removed, especially after extended service. That alone does not prove failure. More concerning findings include a localized sharp bend, a flattened cross-section, an area that will not follow a smooth curve, turn-to-turn overlap, or a point where the component catches against a smooth inspection surface.
Do not repeatedly flex a suspect part to “see whether it recovers.” Repeated manual cycling without a defined radius and load can introduce new damage. Photograph the finding in its received condition and compare it with the applicable acceptance criteria.
Surface Condition and Corrosion
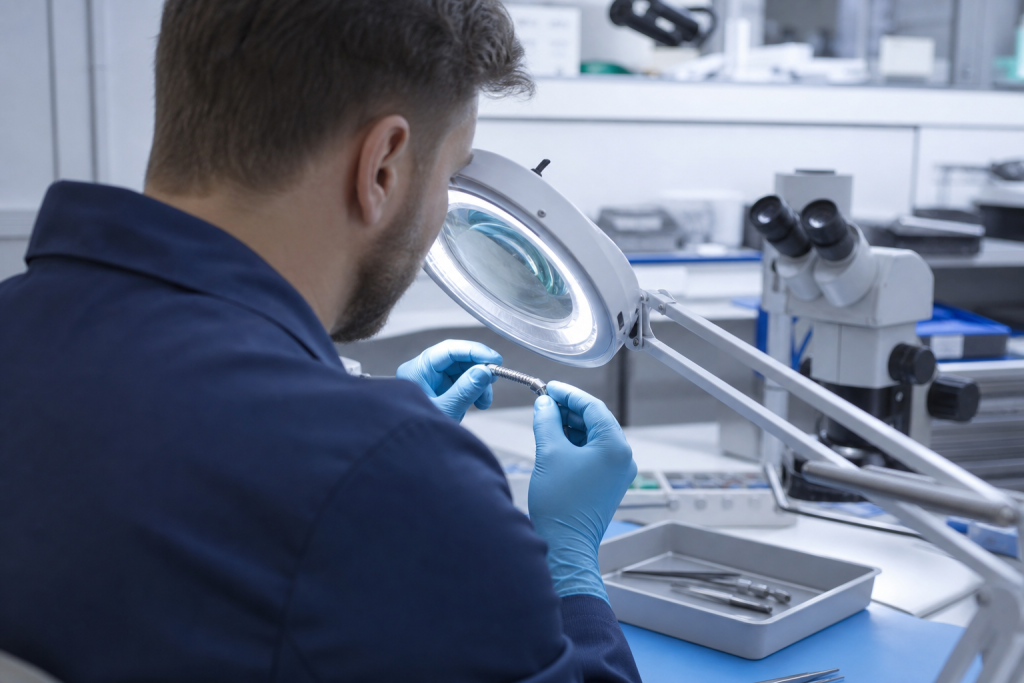
Discoloration is not always corrosion, and a clean metallic appearance does not guarantee acceptable condition. Use appropriate lighting and magnification to check for pitting, roughness, flaking, residue, or changes concentrated near joints. If cleaning is permitted before inspection, use only the approved method and document that it occurred.
Surface damage matters because a rough or raised area can abrade adjacent components during movement. Reject or escalate any condition that cannot be evaluated confidently under the repair center’s documented criteria.
Compare New and Removed Parts Carefully
Place the components on a clean inspection surface without forcing them into the same curve. Compare total length, working length, outer diameter, inner clearance where measurable, end fittings, orientation, and transitions. Any comparison must follow the measurement method and tolerance appropriate to the specific model.
Specifications to Confirm Before Ordering
- Endoscope manufacturer and exact model designation.
- Part name and location within the assembly.
- Overall length and defined working length.
- Outer and inner diameter where applicable.
- Coil pitch, winding direction, and visible construction details.
- End-fitting shape, dimensions, orientation, and attachment method.
- Required material, flexibility, finish, and packaging conditions.
- Photographs of the full part, both ends, and any identifying geometry.
Ask the supplier to confirm that the proposed item is compatible with the stated model. Do not rely on “universal” descriptions unless the dimensional and functional requirements have been independently verified.
How to Build a Clear Coil Pipe RFQ
A good request for quotation reduces the chance of receiving a part that is visually similar but mechanically different. Begin with the exact endoscope model and describe where the coil pipe is located. State whether you need a loose component, a coil with fittings, or a larger preassembled unit. Attach photographs with a scale in the frame, but do not use the photograph as a substitute for numerical dimensions.
Separate required characteristics from preferences. Required characteristics may include diameter, length, end geometry, routing orientation, or material. Preferences might include packaging style or minimum order quantity. This distinction helps the supplier identify what must match and where alternatives may be discussed.
Questions to Ask the Supplier
- Which exact endoscope models has this part been specified as compatible with?
- Are the published dimensions nominal values or controlled tolerances?
- Does the quoted item include all fittings shown in the photograph?
- How is the component protected against kinking and contamination during shipment?
- Is lot or batch information provided for traceability?
- What is the process for reporting a dimensional or workmanship nonconformance?
- Can the supplier provide a pre-shipment photograph or drawing when the model is uncommon?
Terms such as “original,” “OEM,” and “compatible” should be used accurately. A third-party compatible part should not be presented as an original manufacturer part unless that relationship is documented. Clear terminology protects both the buyer and supplier from incorrect assumptions.
Measurement Methods That Reduce Ordering Errors
Flexible parts are easy to measure badly. The repair center should define how the component is positioned, where each dimension begins and ends, and how much contact force is allowed. Two technicians can obtain different values if one straightens the part under tension while the other allows it to rest naturally.
Overall Length Versus Working Length
Overall length may include fittings, while working length may refer only to the flexible coil body or the span between reference shoulders. State the definition next to the measured value. If the removed component is broken or stretched, do not treat its current length as the original specification without corroborating evidence.
Diameter and Inner Clearance
Measure at multiple representative points when the method permits. A single reading may miss taper, ovality, or localized deformation. For an inner feature, use a suitable gauge or verified reference rather than forcing caliper jaws into a delicate opening.
Documenting End Geometry
Photograph each end separately and include a straight-on view plus a side view. Record shoulder-to-end distances, fitting diameter, bore, flats, grooves, threads, slots, and orientation features. If the two ends differ, label them consistently in the RFQ and receiving record.
Incoming Inspection for a Coil Pipe Assembly
Keep the supplier label and lot information linked to the inspection record. Confirm quantity and part identity before opening protective packaging. Under appropriate magnification and lighting, check the coil body, transitions, and fittings for transport damage, burrs, contamination, discoloration, or inconsistent workmanship.
Measure only with suitable, calibrated equipment and an established method. Excessive contact pressure from calipers can distort a flexible component and produce a misleading result. If flexibility or bend behavior is part of acceptance testing, use a controlled fixture and approved limit rather than an improvised hand test.
Sampling and Lot Decisions
Inspection quantity should reflect part criticality, supplier history, lot size, and the repair center’s quality procedure. A first order from a new supplier may justify increased inspection. When a sample fails, follow the defined escalation rule instead of quietly selecting the best-looking pieces from the shipment.
Keep accepted and rejected material physically or electronically separated. Link photographs and measurement records to the supplier lot so a later installation issue can be traced efficiently.
Storage and Handling Before Installation
Store coil pipe assemblies in packaging that prevents crushing, sharp bending, contamination, and mixing of similar variants. A large coil should not be forced into a small bag or secured with a tight tie that creates a permanent set. Use labels that identify the part, compatible model, supplier lot, and inspection status.
At the repair bench, keep the component away from loose abrasive debris, inappropriate chemicals, and tools that can nick the coil. Avoid placing heavier parts on top of it. If protective caps or sleeves are supplied, leave them in place until the installation step that requires removal.
Installation and Post-Repair Controls
Route and secure the assembly according to model-specific documentation. Protect adjacent channels, wires, and optical elements from abrasion, pinching, twisting, or heat. Do not substitute adhesives, soldering methods, or attachment hardware without documented authorization.
After installation, complete the required functional checks for the repaired system. Depending on the model and work performed, this may include movement, insertion-section behavior, leak testing, visual inspection, electrical-safety checks, and reprocessing before release. A part that fits dimensionally is not fully accepted until the repaired endoscope meets the applicable performance and safety criteria.
Avoiding Damage During Routing
Plan the route before securing the component. Check that the coil does not cross a sharp edge, trap a channel, twist a wire bundle, or sit under a fastener. Apply only the bend radius and manipulation permitted by the procedure. If resistance is encountered, stop and identify the obstruction rather than pulling harder.
Final Documentation
Record the installed part, supplier and lot, relevant measurements, technician, repair date, and results of required tests. If a new replacement resolves the original symptom but creates a new movement or fit concern, do not release the endoscope. Reopen the diagnosis and verify that the selected component and installation are correct.
Evaluating Supplier Performance Over Time
Price and lead time matter, but they do not describe the full cost of a component. Track receiving rejects, documentation errors, installation problems, repeat failures, response time, and corrective-action quality. A slightly cheaper part can become expensive when it causes repeated disassembly or delays a customer repair.
Use consistent defect categories so trends can be compared. Examples include wrong variant, length outside specification, damaged transition, kinked shipment, poor finish, loose fitting, contamination, or incomplete traceability. Review the data periodically and update inspection levels or supplier requirements when the risk changes.
Coil Pipe Assembly Ordering Checklist
- Confirm the exact endoscope manufacturer and model.
- Identify the component location and whether fittings are included.
- Define overall length, working length, diameter, pitch, and end geometry.
- Use clear photographs from several angles with reference points.
- Ask for explicit “compatible with” confirmation for the stated model.
- Agree on packaging, traceability, quantity, and nonconformance handling.
- Inspect the shipment before releasing it to repair inventory.
- Install only under model-specific service information and complete final tests.
Frequently Asked Questions
Can coil pipe assemblies be selected by outer diameter alone?
No. Length, inner clearance, pitch, stiffness, end fittings, orientation, material, and model compatibility may all matter.
Is a slightly bent coil automatically unusable?
Not every natural curve is damage, but a permanent kink, flattening, irregular pitch, sharp edge, or failed dimensional check should be evaluated against documented acceptance criteria. Do not straighten the part informally.
What information helps a supplier confirm compatibility?
The exact endoscope model, clear photographs, measured dimensions, end-fitting details, and the function or location of the removed component provide a stronger basis than a general product name.
Conclusion
Ordering a coil pipe assembly requires more than matching a picture. A structured specification covering geometry, flexibility, interfaces, condition, and model compatibility reduces delays and repeat repairs. Browse Endopart’s coil pipe assembly category or contact the team with your model and measurements for compatible-part assistance.
Reference: FDA guidance emphasizes that proper servicing is critical to the continued safety and effectiveness of reusable medical devices. See FDA Guidance: Remanufacturing of Medical Devices.